Business Details
50+ Years
experience
Emergency
services
Your Trusted Partner for Industrial Material Handling Solutions
Gough Econ is a globally recognized leader in the design and manufacture of integrated bulk material handling systems. Headquartered in Charlotte, NC, our 40,000-square-foot facility combines advanced engineering with hands-on testing capabilities to deliver reliable solutions tailored to client needs. Since our founding in 1974, we have prioritized innovation, developing patented technologies that address complex material handling challenges across diverse industries. Our team collaborates closely with process engineers and operational staff to optimize production efficiency while maintaining strict safety and sanitation standards. With a global track record spanning decades, we specialize in custom-engineered systems that maximize throughput, reduce downtime, and enhance profitability.Our commitment extends beyond installation through comprehensive support programs, including preventative maintenance and rapid-response service. Acquired in 2004 by long-time employees David Risley and Don Calvert, our company culture emphasizes employee empowerment and customer partnership. We serve industries ranging from food processing to pharmaceuticals, ensuring compliance with SQF, OSHA, and other regulatory frameworks. Our mission remains focused on delivering value-driven solutions that align with both client objectives and operational realities. This dedication to excellence has solidified our reputation as a trusted partner for large-scale industrial projects worldwide.
Services
Bulk Material Handling
Conveyor Systems
Integrated Systems
Preventative Maintenance
Custom Equipment Design
On-Site Support
Parts Replacement
System Reconfiguration
Sanitary Design
Automation Solutions
Details
- Year established: 1974
Highlights and features
- We offer over 43 years of specialized expertise in bulk material handling systems.
- Our patented multi-axis bucket conveyor technology enables directional flexibility unmatched in the industry.
- We provide preventative maintenance programs to control costs and avoid unscheduled downtime.
- Our engineers collaborate directly with clients to develop custom solutions for unique production challenges.
- We maintain a global track record of successful installations across food, pharmaceutical, and industrial sectors.
Services
Integrated Systems
Our integrated systems combine conveyors, bucket elevators, and control networks into cohesive solutions tailored to production workflows. These systems optimize material flow from raw input to packaged output while reducing manual handling. Designed for industries requiring high throughput and reliability, our engineering team ensures seamless compatibility between components to maximize efficiency and minimize maintenance requirements.
Bulk Material Handling
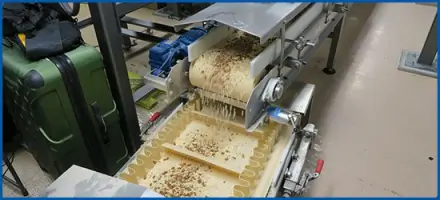
Custom-engineered bulk material handling solutions address challenges in transporting powders, granules, and solid materials across diverse sectors. Our equipment incorporates features like multi-axis movement and automatic cleaning to maintain product integrity. Systems are designed for heavy-duty applications while meeting safety and sanitation standards required in food and pharmaceutical manufacturing environments.
Conveyor Systems
We manufacture a full range of conveyor systems including belt, vibratory, and bucket conveyors for horizontal and vertical material transport. Our designs accommodate specialized needs like sanitary processing and high-capacity throughput. Modular configurations allow adaptation to existing facilities while maintaining operational efficiency and ease of maintenance.
Preventative Maintenance
Our preventative maintenance programs reduce unscheduled downtime through scheduled inspections and component replacements. Technicians provide detailed reports after each service visit, identifying potential issues before they impact production. Customizable plans available for quarterly, semiannual, or annual support tailored to specific system requirements.
Custom Equipment Design
Custom equipment design services focus on solving unique material handling challenges through patented technologies and innovative configurations. Our engineers collaborate with clients to develop solutions that optimize floor space, improve safety, and enhance system longevity. This includes specialized features like multi-discharge points and heavy-duty construction for demanding environments.
People
David Risley
Co-Owner
Co-owner with extensive industry experience since joining Gough Econ in 1978. Instrumental in transforming the company into a global leader through strategic acquisitions and operational improvements.
Don Calvert
Co-Owner
Co-owner who helped transition Gough Econ from UK ownership to independent US operation in 2004. Focuses on maintaining engineering excellence while expanding the company's global market presence.
Clint Gamage
Customer Support Manager
Manages technical support operations with over 15 years of experience in industrial equipment maintenance. Specializes in optimizing system performance through preventative maintenance strategies and rapid-response service solutions.
Ben Morris
Customer Support
Provides on-site technical assistance with expertise in conveyor system diagnostics and repair. Focuses on minimizing production downtime through efficient troubleshooting and parts replacement services.
Questions
What industries does Gough Econ serve?
We serve food processing, pharmaceutical, chemical, and industrial manufacturing sectors requiring bulk material handling solutions.
Do you offer custom equipment designs?
Yes, our engineers develop customized systems tailored to specific production requirements and facility constraints.
What maintenance support options are available?
We provide preventative maintenance programs with customizable schedules and on-demand repair services.
Can your systems integrate with existing equipment?
Our solutions are designed for compatibility with both new and legacy systems to optimize overall efficiency.
How do you ensure product safety in food handling?
Our sanitary designs meet SQF standards with features like automatic cleaning and stainless steel construction.
What makes your bucket conveyors unique?
Our patented multi-axis technology allows directional flexibility unmatched by conventional conveyor systems.
Reviews (4)
Amit & Neelam Mehta
Feb 06, 2021
Report
Best bucket elevator manufacturer. Super nice people who know what they are doing. Have been working with them over 10 years.
Mirsad Imsirovic
Dec 24, 2019
Report
As a trucking company it is nice to see there are still understanding shippers out there. Quick In and Out
IPhoneUser
Jan 21, 2018
Report
These guys really know what they are talking about. We have been going business for over a year and I can personally recommend them.
Joseph Pennington
Sep 13, 2016
Report
Smart and insightful people make a great product for careful and safe handling of fragile food. Check 'em out.