Business Details
50+ Years
experience
Durable Industrial Rotary Pumps Manufacturer Since 1938
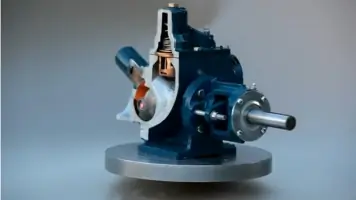
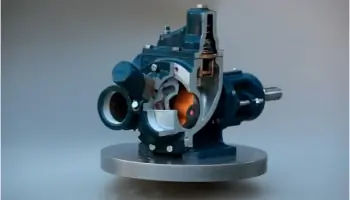
Granco Manufacturing has been a trusted leader in the design and production of rotary ball pumps since 1938. Our commitment to innovation and quality has established us as a premier manufacturer of durable, high-performance pumping solutions for demanding industrial applications. Our unique floating rotor design eliminates metal-to-metal contact, ensuring unmatched longevity and efficiency in harsh environments. With a global customer base spanning petroleum, food processing, and chemical industries, we deliver adaptable pumps capable of handling viscosities from 32 SSU to over 1,000,000 SSU. Our in-house engineering expertise and Made-in-the-USA manufacturing standards guarantee precision-crafted products that meet rigorous industry requirements. We maintain extensive inventory for same-day shipping from our Caldwell, Idaho facility while providing personalized technical support to optimize pump performance for specific operational needs.Our Ni-Resist alloy pumps offer superior corrosion resistance comparable to stainless steel without galling issues, serving critical applications in marine, chemical, and food handling sectors. Decades of continuous improvement have refined our reversible flow technology, enabling effortless directional adjustments through simple valve rotation. As an industry pioneer, we invest in advanced hydraulic drive systems that deliver precise flow control for complex plant operations. Our comprehensive service portfolio includes custom pump configurations, system integration, and technical consultation to address unique fluid transfer challenges. Every Granco pump embodies our founding principles of reliability, engineering excellence, and customer-centric innovation that have defined our 85-year legacy.
Services
Rotary Ball Pump Manufacturing
Custom Pump Solutions
Technical Support
Same-Day Shipping
Hydraulic System Integration
Details
- Year established: 1938
Highlights and features
- We offer 85+ years of specialized expertise in rotary pump engineering
- Our patented floating rotor design reduces wear and extends pump life
- We guarantee same-day shipping for standard pumps and parts
- Our Made-in-the-USA manufacturing ensures strict quality control
- Our pumps handle viscosities from 32 SSU to over 1,000,000 SSU
Services
Rotary Ball Pump Manufacturing
We engineer and produce rotary ball pumps designed for demanding industrial applications. Our patented floating rotor technology ensures exceptional durability and efficiency across extreme operating conditions. These pumps deliver reliable performance in petroleum transfer, chemical processing, and food industry applications requiring versatile fluid handling capabilities.
Custom Pump Solutions
Our engineering team develops customized pump configurations to meet specific operational requirements. We provide specialized solutions for challenging applications including high-viscosity transfer, hazardous environment operations, and integrated hydraulic systems. Our experts ensure optimal pump selection and configuration for unique industrial processes.
Technical Support
We offer comprehensive technical guidance for pump selection, installation, and maintenance. Our experienced support team provides application-specific recommendations and troubleshooting assistance. We maintain detailed specifications and performance data to ensure proper pump system optimization for customer operations.
Same-Day Shipping
Our extensive inventory enables immediate shipment of standard pump models and replacement parts. We maintain ready stock at our California distribution center to facilitate urgent deliveries. This service ensures minimal downtime for customers requiring prompt equipment replacement or expansion.
Hydraulic System Integration
We design and implement complete hydraulic pumping systems for industrial fluid management. Our HY-DRIVE technology enables precise flow control and reversibility in complex plant operations. These integrated systems optimize efficiency in bulk transfer applications across multiple production points.
Questions
Are Granco pumps suitable for food industry applications?
Our pumps can handle food products prior to cooking but are not certified as food grade equipment.
What warranty coverage do you provide?
We offer a one-year warranty covering defects in materials and workmanship for all pumps.
What shipping options are available?
Standard pumps ship same-day with next-day delivery available for urgent requirements.
Can your pumps handle high-viscosity fluids?
Our pumps transfer fluids ranging from 32 SSU (water) to over 1,000,000 SSU (cold grease).
Where are your manufacturing facilities located?
All pumps are manufactured at our Caldwell, Idaho facility with additional operations in California.
Videos